Machine shop
Cycle time from the controller.Read live, while the part is on the machine.
eManage AI reads each CNC, VMC, and HMC from its controller and checks the cell from the camera above it. Run state, spindle hours, part count, and unattended time land on the job card while the part is still on the machine.
For machine shops, eManage AI reads CNC, VMC, and HMC controllers and existing CCTV, then posts cycle time, spindle hours, part count, and idle time to the eManage job card.
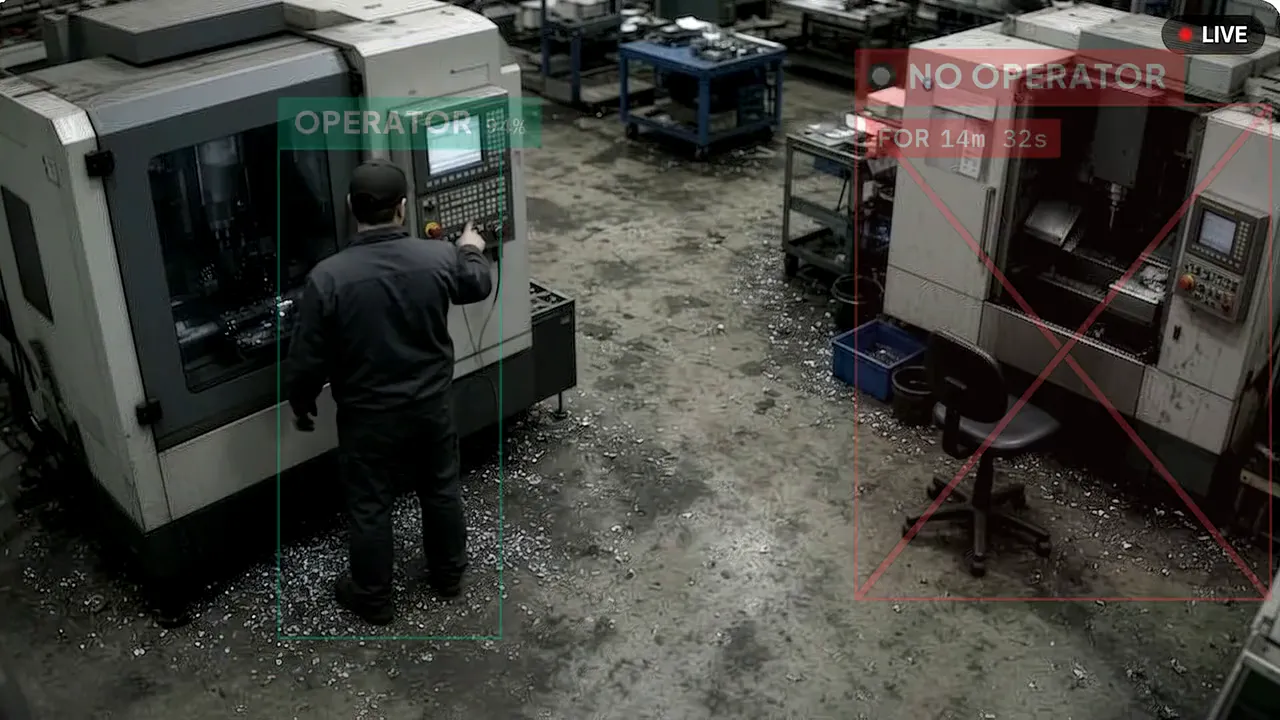
Hidden idle
Running, with nobody there
The controller says running while the operator is at the next machine.
Mixed OEMs
Three brands, three screens
Fanuc, Siemens, and Haas cells never share one shop-floor view.
Typed OEE
Hours keyed at shift end
Cycle hours are typed after the parts have already gone to inspection.
The flow
From bar stock grn to packing and dispatch.One ledger watching every stage.
Today
Bar stock invoices are retyped by hand.
AI on this stage
Document AI →With eManage AI
Invoice lines checked against the PO before posting.
AI for machining: cnc, vmc & hmc
The modules that fit.
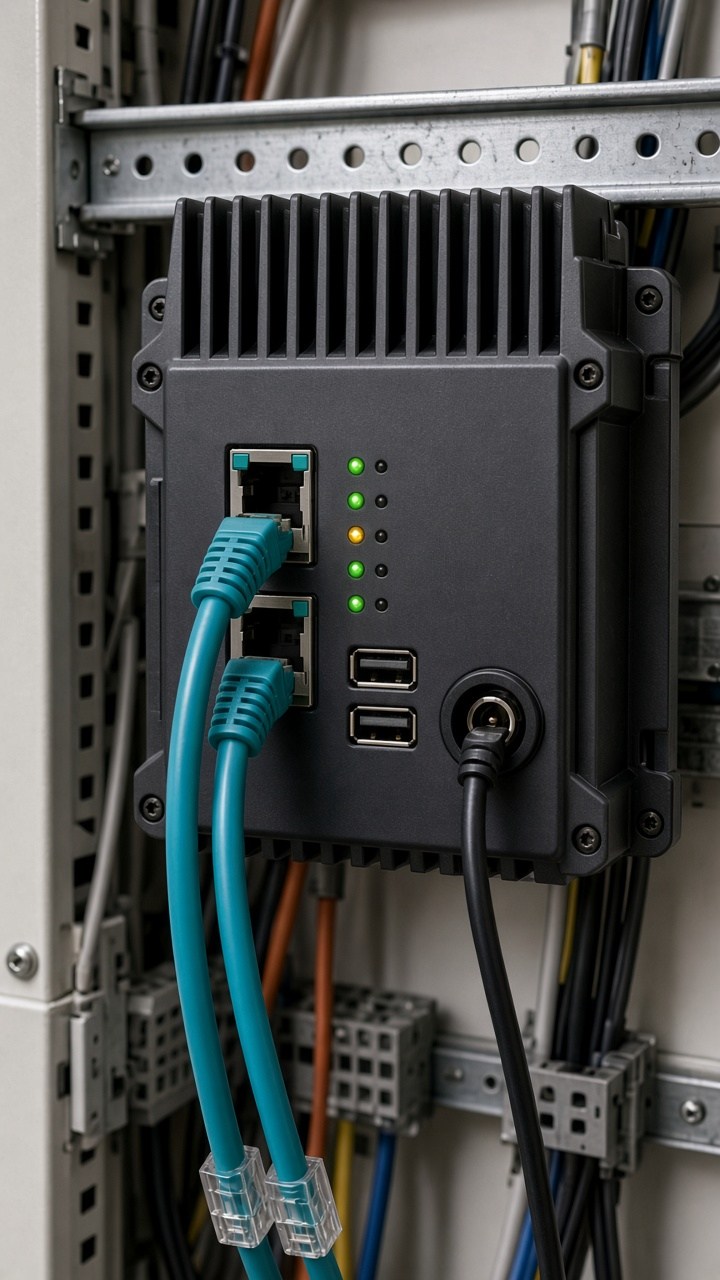
Telemetry
IIoT Edge AI
Reads machine data on a small box inside the plant, and keeps it for up to 72 hours if the internet drops.
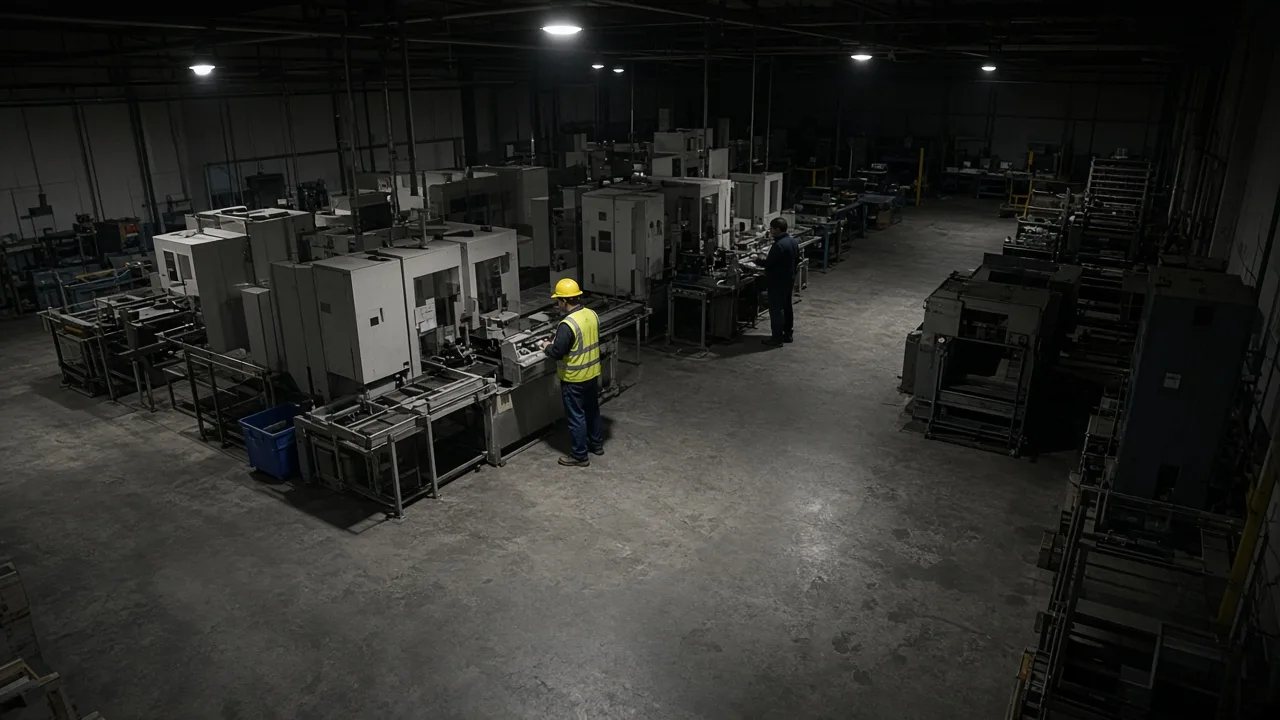
Plant CCTV
CCTV AI
PPE checks and short-stop tracking from your existing cameras, posted to the job card.
Agent
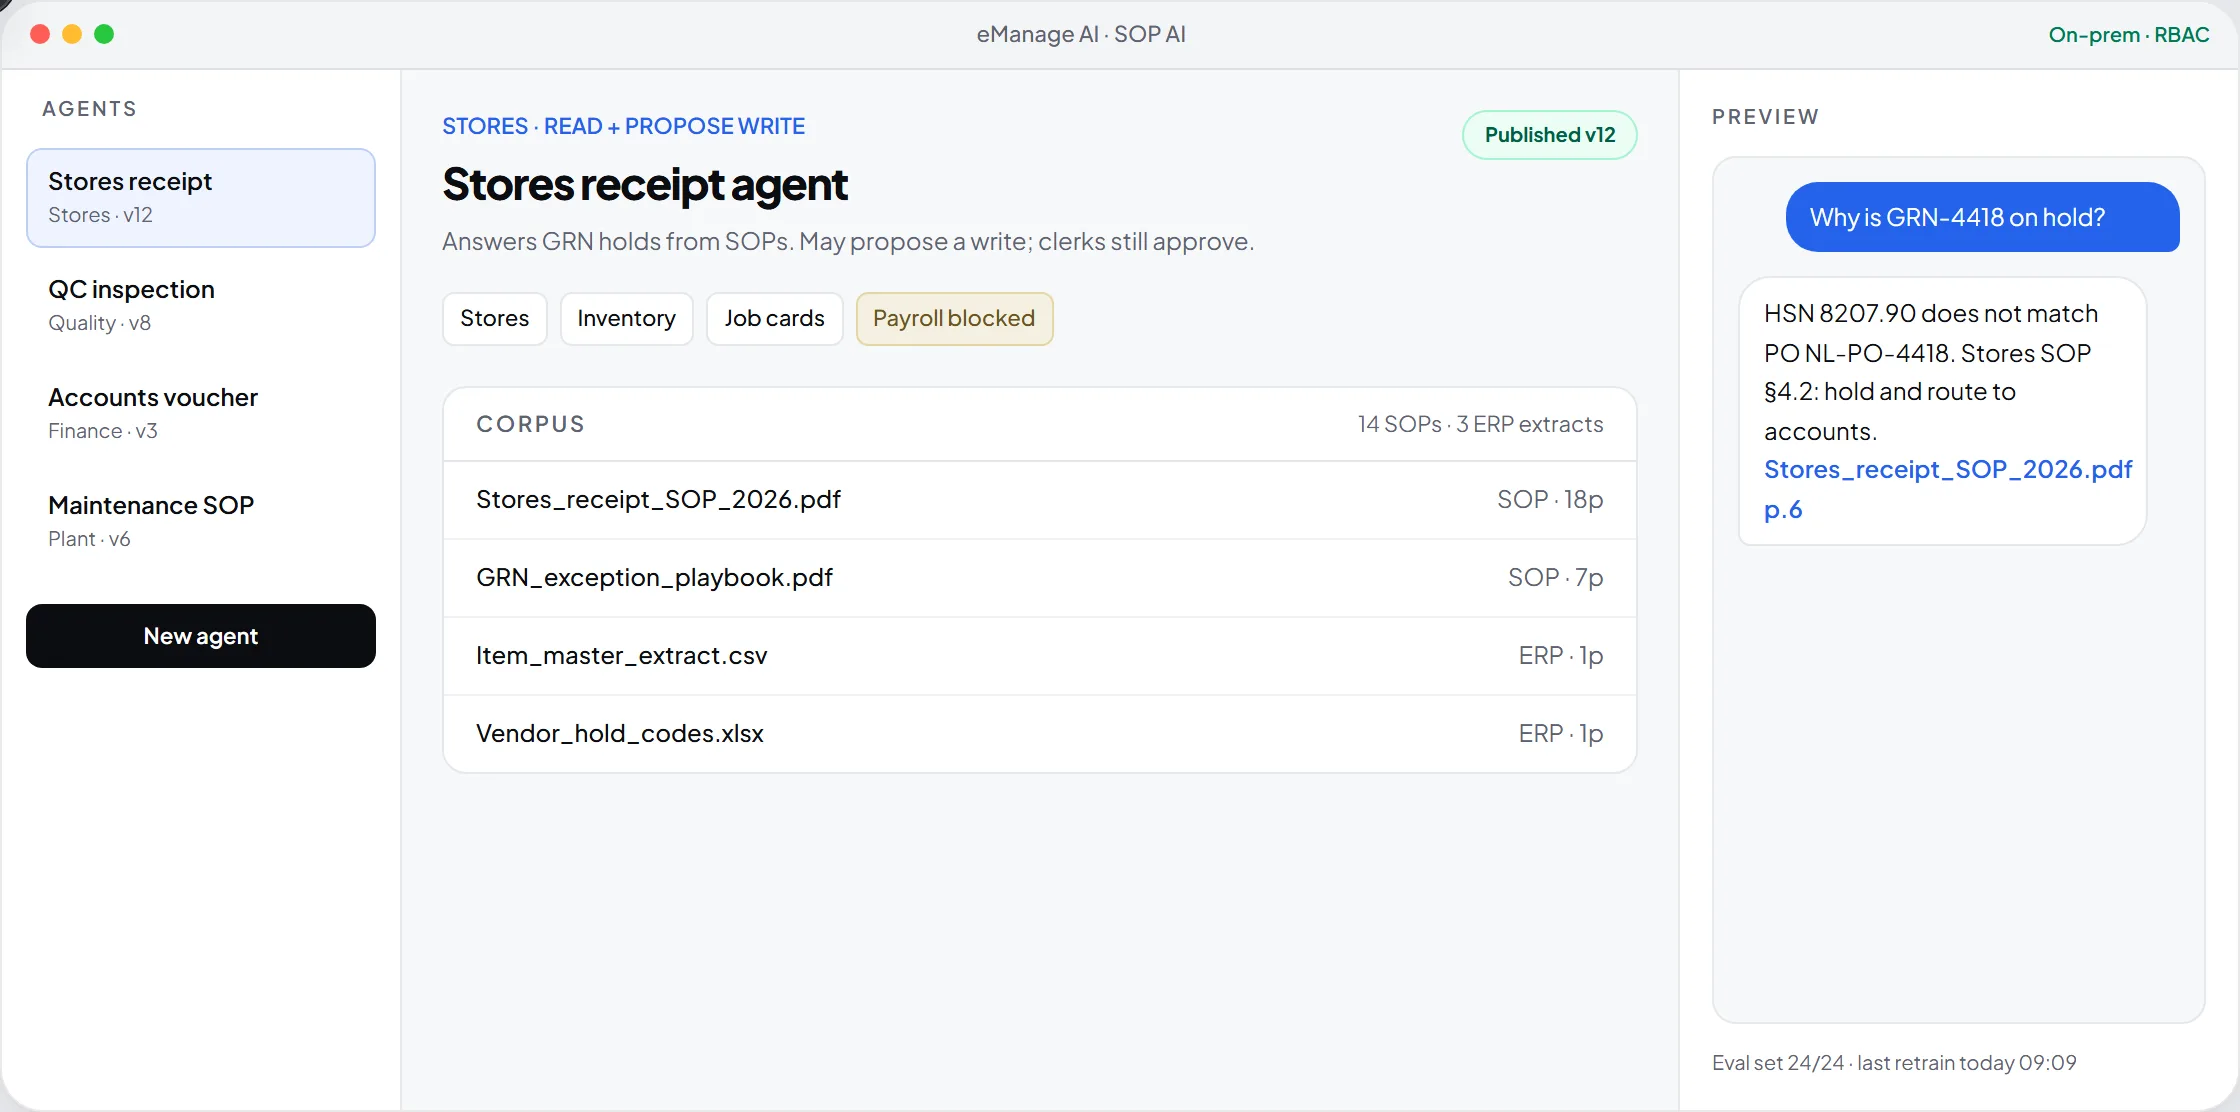
SOP AI
Plant agents that answer from your SOPs, recipes and work instructions, each limited to its own files.
Agent
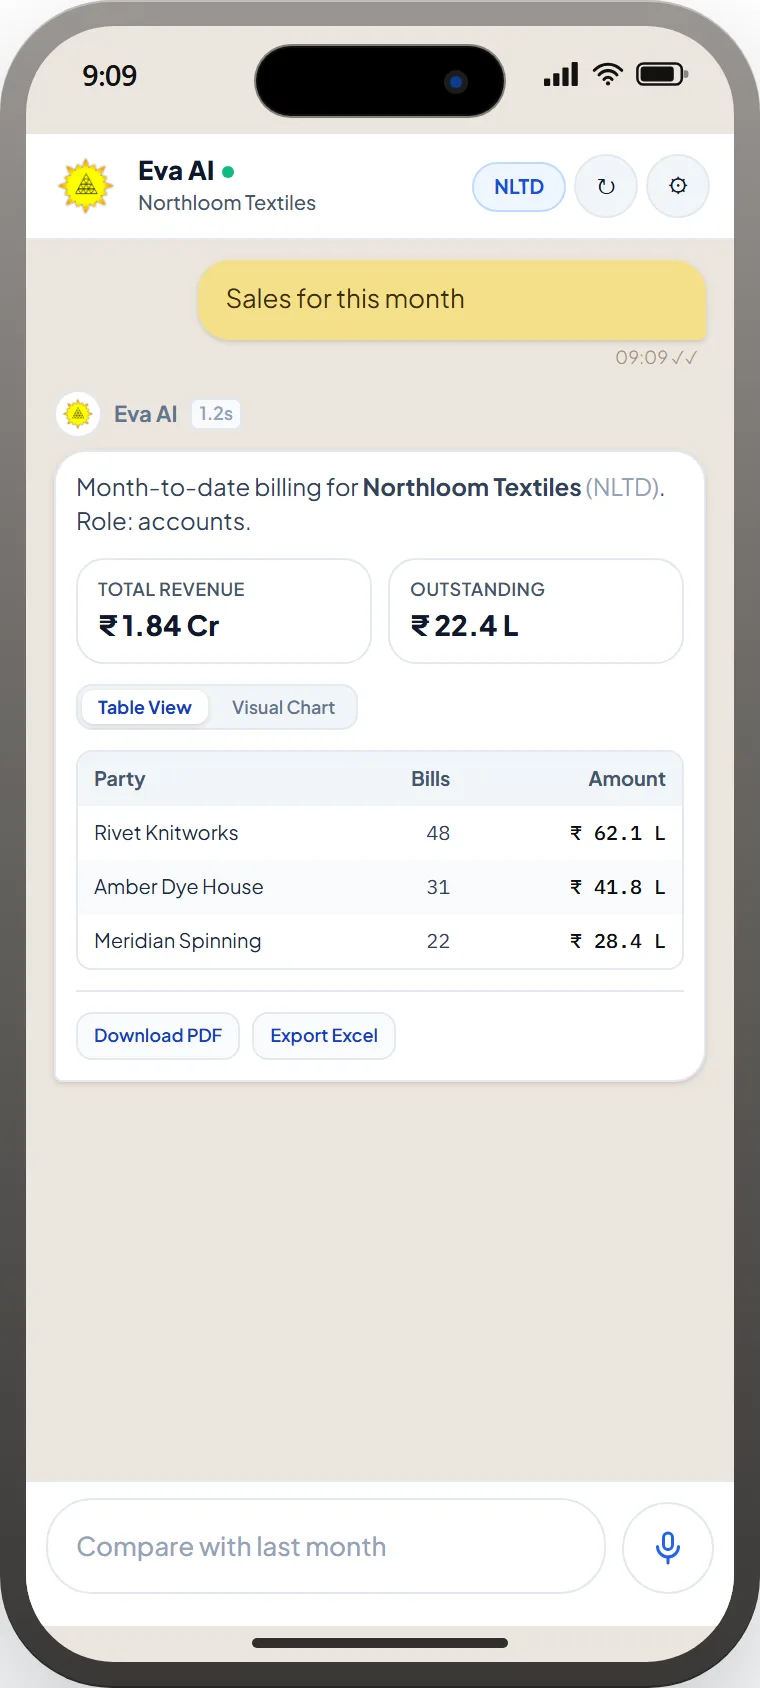
Eva AI
Ask questions in plain English and get answers from live ERP tables, within your login rights.
Agent
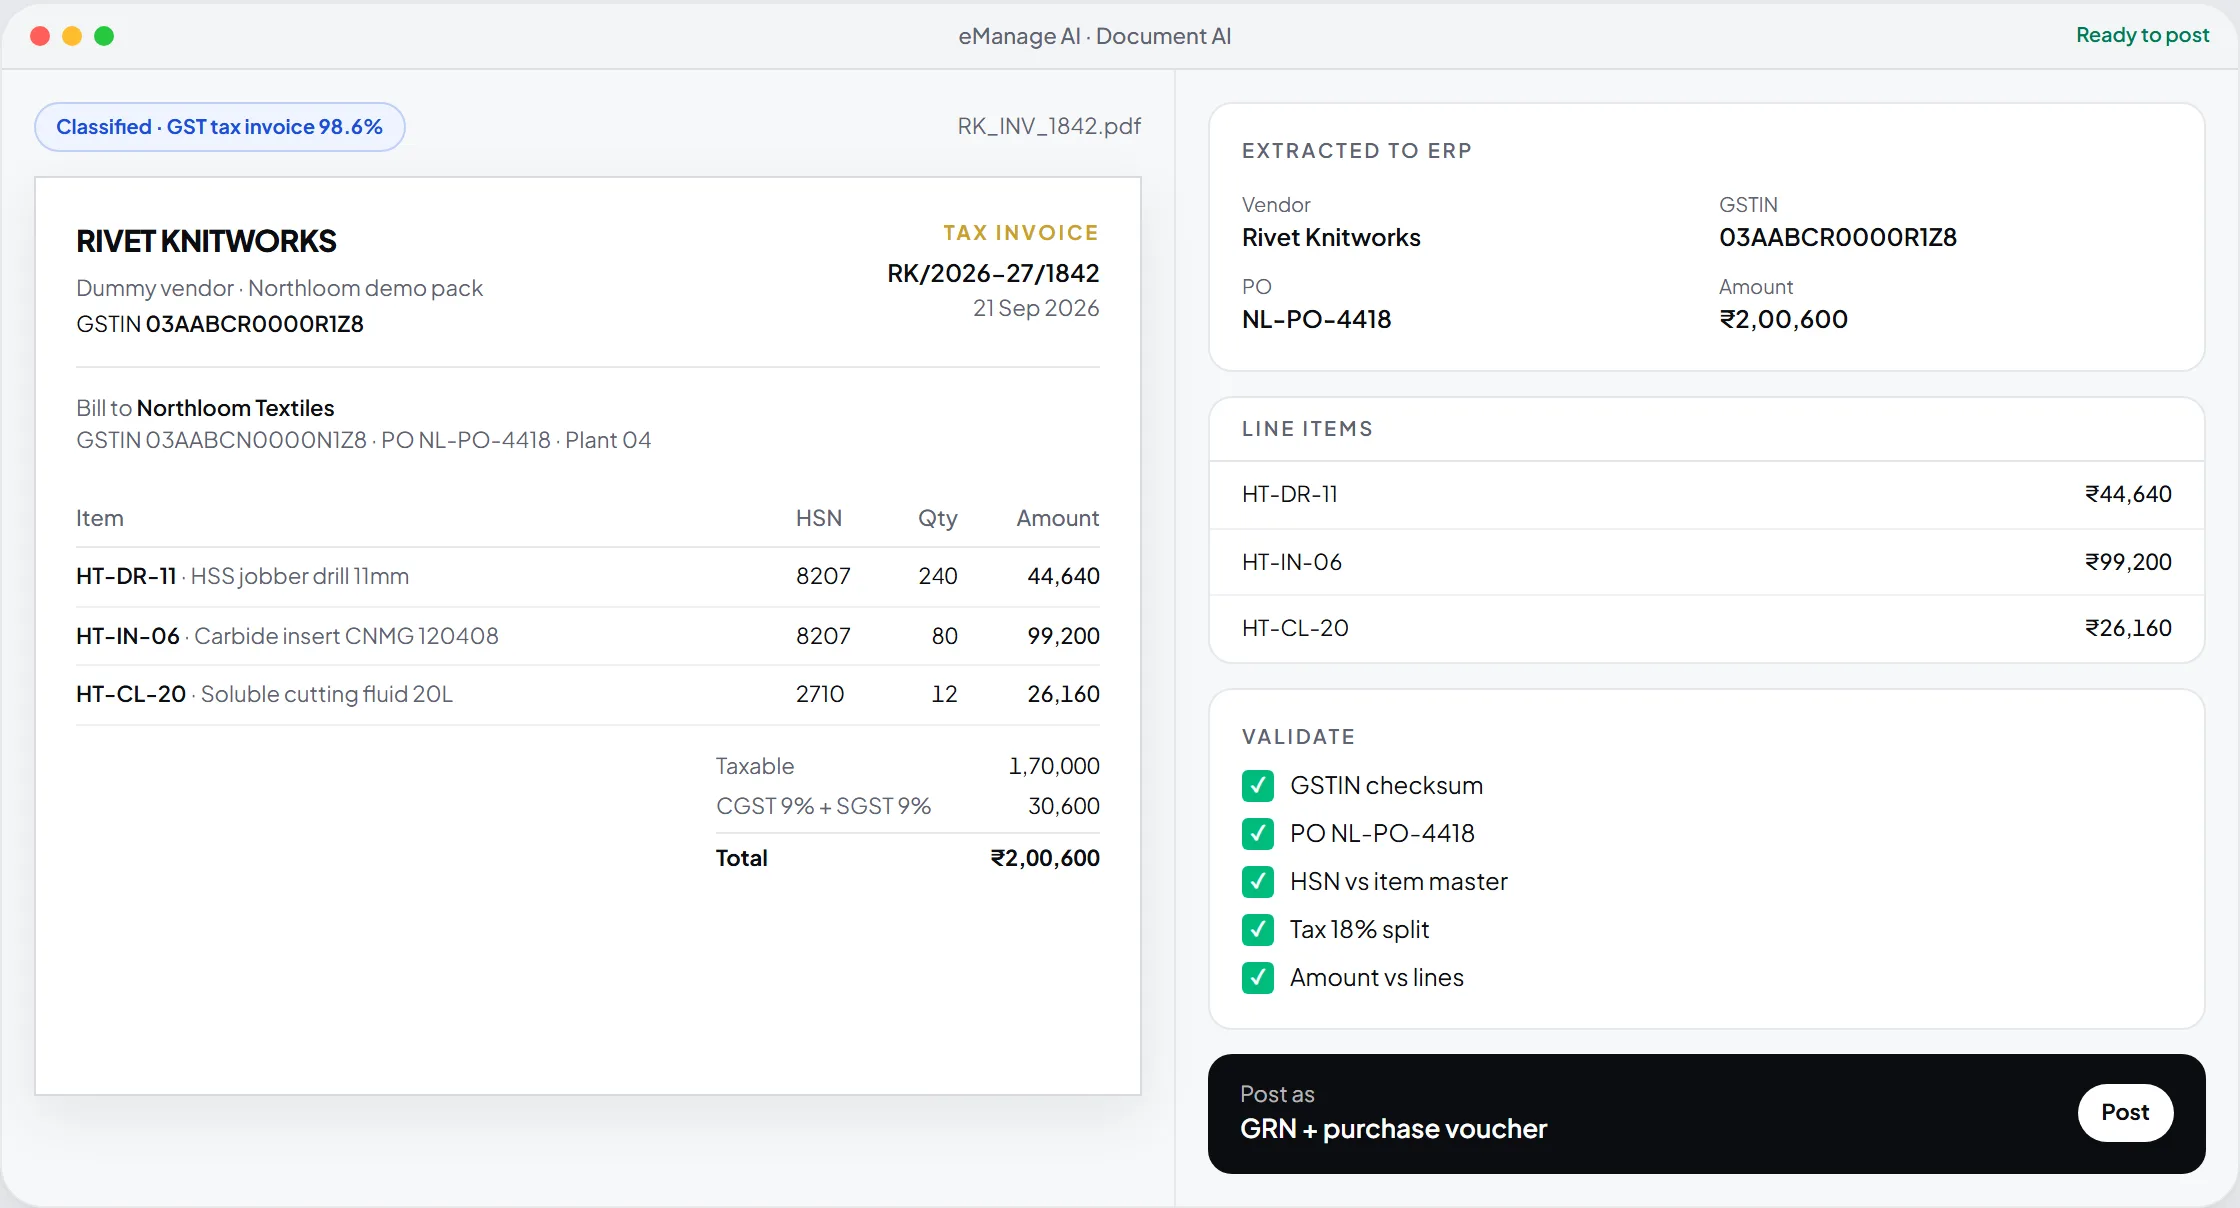
Document AI
Reads invoices, POs, GRNs and KYC papers, checks them, then posts to ERP or holds mismatches.
Demo clips
Watch it count.
Activity & micro-stops
Operator at one cell, the next unattended and timed. The machine controller still calls it ‘running’.
Questions engineering plantsactually ask.
Fanuc, Siemens, Haas and other CNC, VMC, and HMC controllers, including older machines through a small connection box.
No. Operators still start and stop the cycle at the machine. eManage AI reads the controller and writes the job card.
From the camera. CCTV AI watches the cell from an existing camera and times the period with no operator present, even when the controller reports running.
Monitoring carries on. The box in the plant keeps run and stop records for up to 72 hours.
More in engineering
What could your plantrun better?
A feasibility audit maps the cameras, machines and eManage modules you already run, then picks one place to go live.
Book a feasibility audit →