Textile · spindles, looms & knit cells
Mill data, kept in the mill.Ring frames, looms and knit cells, summed up.
eManage IIoT Edge AI reads spindle, loom and knit-cell signals on the mill floor, stops a machine at once on a yarn break or tension fault, and sends machine averages and department OEE to eManage ERP instead of every raw reading.
Stops
Live
Stop signals on site
Offline
72 h offline
Data kept if internet drops
Machines
Old & new
Even without a network port
Internet
90–98% less
Summaries sent, not raw
Raw streams
Thousands of spindles, no usable number.
Spinning and weaving floors produce more signal than the internet link or the cloud should carry. Old frames have no network port at all.
Thousands a minute
Readings from one frame
One ring frame sends thousands of readings a minute.
Instant
Stops cannot wait
A yarn-break or tension stop cannot wait for the internet.
No network port
Older frames and looms
Many machines have only old wiring, with no network port.
On the box
Four monitoring lines. One edge write-back.
Same gateway, same 72-hour buffer. Knit cells, looms, sewing lines, and machining centres each have their own console on the same edge path.
Circular & flat knit
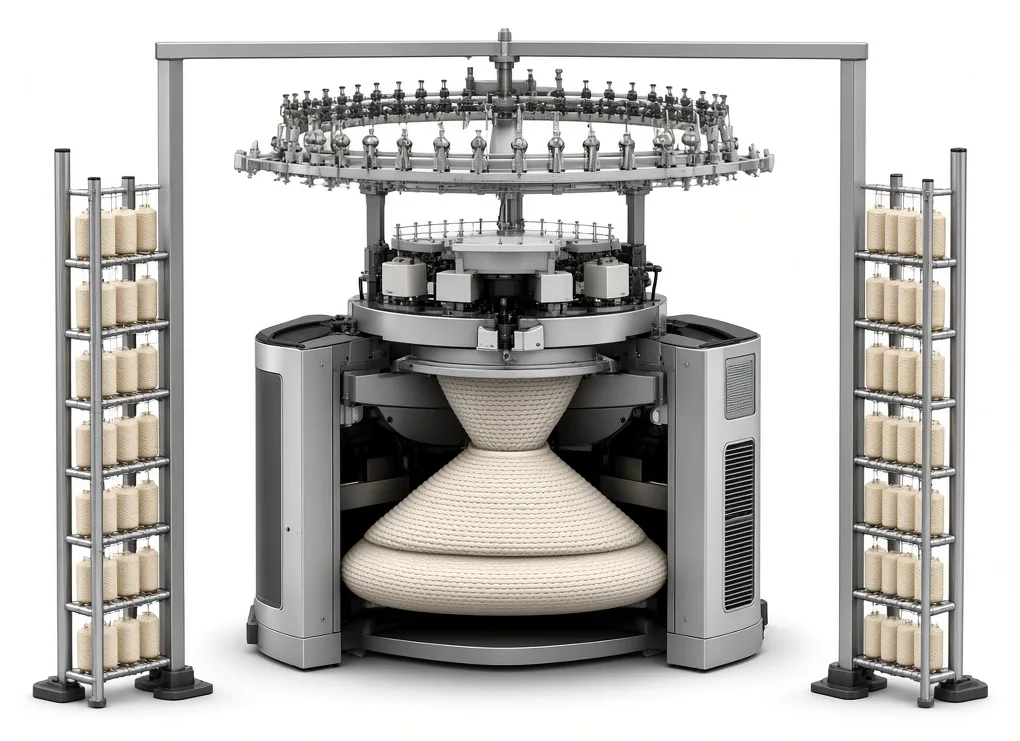
Knitting Monitoring AI
Speed, yarn breaks and stop reasons from every circular or flat knitting machine reach the live job card as they happen. No clipboard at shift end.
- Yarn-break and needle-line stops
- Speed against the job ticket
- Keeps data if the internet drops
Looms & weaving sheds
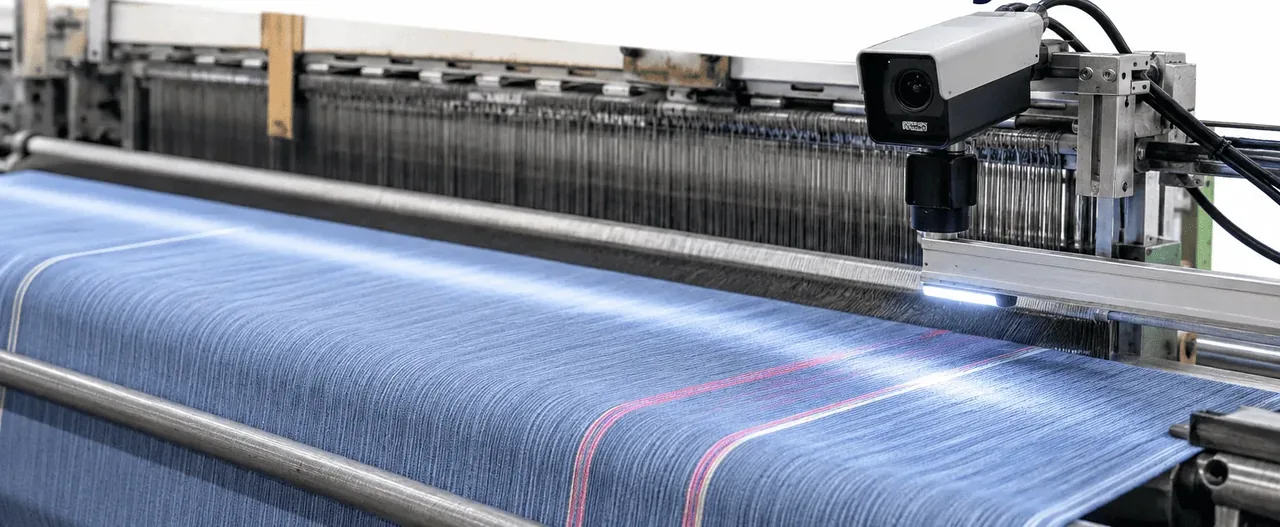
Weaving Monitoring AI
Every loom's counter and stops are read live. Opening and closing readings, net metres and weaver averages fill the Day and Night shift report, with no walk round the shed with a pen.
- Net metres and kg per loom, per shift
- Warp, weft, beam, and fitter stops with minutes
- Production, finishing, and fabric stock in the ERP
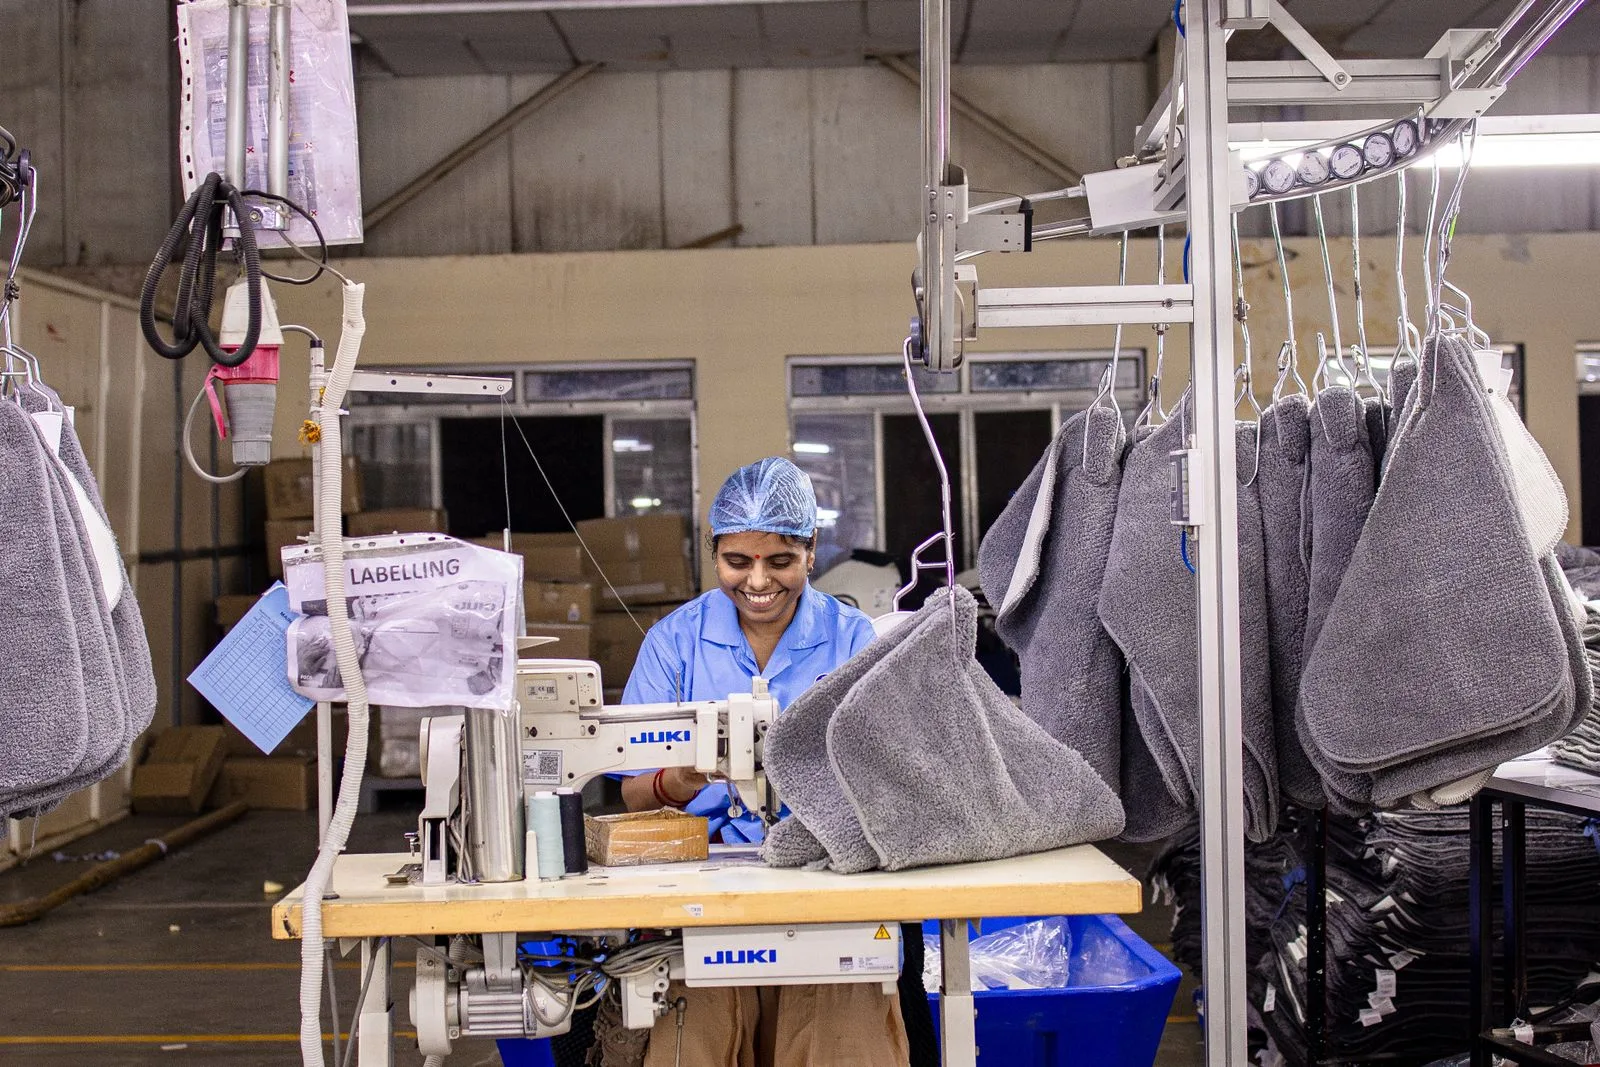
Garment sewing lines
Sewing Monitoring AI
Servo-motor taps and clamp-on sensors stream SPM, needle time, and idle reasons from every station. The hour-by-hour board and the bundle card update while the style is still on the line.
- SPM and needle time per station
- Bottleneck and WIP flagged live
- Piece-rate and DHU on the bundle card
Machining centres
VMC / HMC / CNC Monitoring AI
Cycle time, axis load, idle, and spindle hours sync to the same job card as the rest of the plant. Device tiles, gauges, and last-known values share one shop console.
- Cycle, idle, and micro-stops
- Tool-load and spindle hours
- Job-card write-back, not a second HMI
How it connects
What runs at each hop.
Data moves in steps from the machine to the head-office ERP. The gateway links each step on site.
Plant
Gateway to plant and cloud
Carries spindle speed, picks and power over an encrypted link. Fast enough to stop a machine.
Machines
Machine to gateway
Works with machines such as Rieter, Picanol, Murata and Toyota. Readings are encrypted and checked.
Older
Older machines & meters
Connects older spinning and carding machines and energy meters. Runs on a separate network, isolated from the office.
ERP
ERP & report sync
Hourly totals, tickets and inventory post to eManage in batches. This link does not control machines.
How it works
Four moves.One write-back.
- 01
Connect the machines.
Old and new machines connect to one small box.
- 02
Act on the floor.
Stop and tension alarms act at once, inside the plant.
- 03
Filter to averages.
Raw spindle and loom readings become machine averages and department OEE.
- 04
Sync to eManage.
The box keeps up to 72 hours of data if the internet drops. Alarms sync first, then the rest.
Four-tier edge
Where the millisecond lives
T1
Machine
Sensors and the machine's own controller.
T2
Plant box
Reads every machine live. Keeps 72 hours if the internet drops.
T3
Plant
Shed screens, line totals, local alarms.
T4
ERP
Totals post to eManage ERP; details follow.
Inside eManage ERP
One set of numbers for payroll and production.
Shift efficiency and stop reasons post to job cards. Piece-rate and OEE come from the same data, so the two figures agree.
- Rieter, LMW, Schlafhorst, Picanol and Sulzer machines in one plant model
- Data encrypted on the box and on the way to eManage
- Separate network, USB ports disabled, locked box
Four tiers
Tier 1 — machine
Sensors on the frame for spindle speed, loom picks and warp tension. Standard industrial sensor wiring.
Tier 2 — cell gateway
Rugged gateway per department that keeps 72 hours of data.
Tier 3 — plant
A server in the plant for yarn-break prediction, shed OEE and the operator screen.
Tier 4 — ERP / HO
eManage sync, multi-plant totals and long-term machine data storage.
Questions plantsactually ask.
Speed and cost. Machine stops must act at once, and sending every spindle reading costs money. The box turns them into machine averages and department OEE first.
Local alarms and checks keep running. The box keeps up to 72 hours of data, and when the internet returns alarms go first, then the rest.
Yes. A small box connects them, so old and new machines show on the same screens.
Physical locks, a separate machine network, disabled USB ports, encrypted storage and encrypted links checked for each device.
What could your plantrun better?
eManage IIoT Edge AI reads spindle, loom and knit-cell signals on the mill floor, stops a machine at once on a yarn break or tension fault, and sends machine averages and department OEE to eManage ERP instead of every raw reading.
Map your machine list →Next